
Parts & Field Service
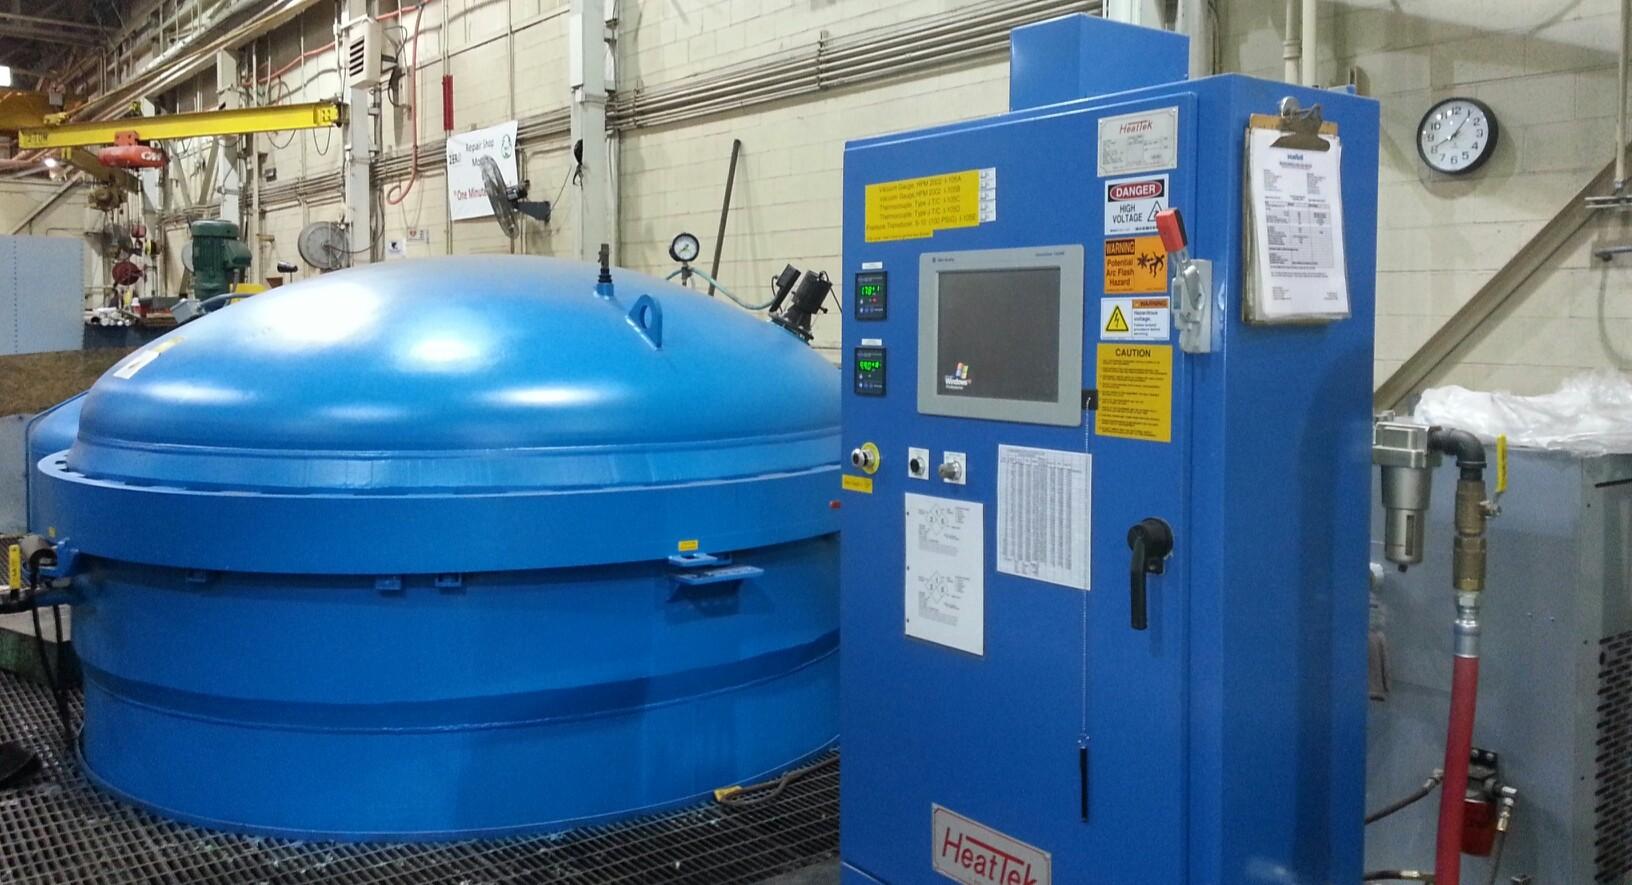
The Parts and Field Service Teams at HeatTek understand your equipment and operations. From ovens to washers to impregnation systems, we’ll be your trusted partner to provide the parts and service you need quickly, efficiently and cost-effectively.

PARTS and SERVICE OPTIONS



Why Customers ChooseHeattek
Custom-Engineered Solutions
Every system is built from the ground up to match your exact process requirements.
Industry-Specific Expertise
Expertise in our core industries enables us to deliver precisely what each customer needs.
A Proven Design Process
A collaborative, end-to-end approach built for long-term performance and ROI.
Ongoing Support Beyond the Build
HeatTek provides lifetime service and support—from parts to training—beyond just equipment delivery.
HOW CAN HEATTEK SUPPORT YOUR EQUIPMENT IN THE FIELD?
Click on one of the links below to learn more about the services we offer, to buy spare parts or to see what retrofit options may be available to you. We support equipment made by any manufacturer - even if it's not HeatTek!
Heattek FAQs
Yes. You can pick it up at: HeatTek - Plant 2, N8135 Industrial Drive, Ixonia WI 53036
Yes, we do. Many of the same parts used on our equipment will directly cross over to your existing equipment built by other manufacturers. If it is not a direct fit, our Parts Sales Specialists will be happy to assist you in locating the correct part that will get you back up and running.
An industrial oven should be cleaned regularly based on usage, typically with light cleaning done weekly and more thorough maintenance performed monthly or quarterly. High-use or high-contamination applications may require more frequent cleaning to prevent buildup, maintain efficiency, and ensure product quality.
Yes. HeatTek's training staff is available to teach your operators how to properly and efficiently use the equipment at the highest levels of safety. This includes reviewing the operating instructions and providing an overview of routine and preventative maintenance so you can get the most out of your new purchase. Contact HeatTek for more information.
Yes. HeatTek's training staff is available to teach your operators how to properly and efficiently use the equipment at the highest levels of safety. This includes reviewing the operating instructions and providing an overview of routine and preventative maintenance so you can get the most out of your new purchase. Contact HeatTek for more information.
CUTTING INSTRUCTIONS
1. When splicing the fiber belt care must be taken to assure that the splice is square. Overlap the ends of the belt and align the right edge and the left edge of both ends to be cut. Figure 1 below shows the belt edges out of alignment. If the edges are not aligned and the splice cut is not square, the belt will not track properly once the splice is completed

Note: Belt is not square. If cut and spliced at point A, it will not track properly.
2. Securely clamp both ends of the belt on a flat firm surface. Cut the belt along a straight edge between the securely clamped ends. Allow enough belt so the ends can be overlapped 1-1/2 to 3 inches for the splice. See Figure 2. With the edges aligned, the weave across the width of the belt will not be in line with each other. A square cut does not require alignment of the weave. The cut may be through several rows of weave.

3. In order to cut the belt, square the right edge and left edge of both ends to be cut must be parallel. Don’t be concerned if the lines across the width of the belt align. The square cut may cross several rows across the width. When the cut is made, there should be enough slack in the belt to overlap the cut edges 1-1/2”.
4. When the edges of the belt are square, clamp across the full width of the belt at points B and C. The belt between B and C must be tight enough so the cut along line A is straight. After making the cut, loosen either clamp B or C and overlap 1-1/2”. B
SPLICING INSTRUCTIONS
1. Once the square cut has been made, mark the location of the edges of the belt and loosen one set of clamps.
2. Place the insulation board on a flat, stable surface under the end of the belt to be spliced.
3. Place a layer of the silicone release cloth on top of the insulation board.
4. Place the first layer of belt to be sealed on the release sheet with the side to be sealed facing up.
5. With a felt tip pen, draw a line across the width of the belt depicting the length of the overlap. This will aid in maintaining belt squareness when preparing to heat tack the belt.
6. Place a section of the Teflon PFA film cut to the dimensions of the seal (1”, 1-1/2”, 2”, etc. X belt width) on the surface of the area to be spliced. (Typically .005” thick film unless otherwise specified). Masking tape may be used on each end of this strip to hold the PFA film in position. Do not apply masking tape to the surface to be sealed because the residue of the glue on the masking tape may contaminate the surface to be sealed.
7. Place the second layer to be spliced with the surface to be sliced facing down against the PFA film.
8. Square up the edges using the felt pen marks on the first layer belt surface as a overlap and squaring guide to square the two belt edges.
9. Re-clamp the upper belt so there will be no tension at the splice as the seal is being made.
10. Place the second silicone release cloth over the area to be sealed. 11. Be sure the belt ends to be spliced are held securely in place on both sides of the area to be spliced to prevent movement of the seam during the heat splicing operation.
Note: Be sure the warp of the belts do not lie on top of each other. They must lie beside of each other as shown in Figure 3.

Note: When splicing, align warps next to each other, not side-by-side.
HEATING INSTRUCTIONS
Note: With the belt overlapping seam square and secure, you are ready to heat splice the seam.
1. Check the layers to be sure all components are present. Top layer is silicone release sheet. The second layer is the first surface of the belt to be spliced. The third layer is the PFA film used to make the splice. The fourth layer is the second surface of the belt to be spliced. The fifth layer is the underside silicone release cloth. The sixth layer is the insulated board used to make a solid surface on which to splice the belt. See Figure 4
LAYERING OF MATERIALS PRIOR TO HEAT SEALING

2. When sealing using a heating unit that does not cover the full width of the belt you must start in the center of the belt and work toward the edges as shown. Please see Figure 5 below. Seal in Position 1 first, then move to Position 2, overlapping Position 1 by 1” to 1-1/2”.
3. Continue the process alternating sides and overlapping until the full width of the belt is sealed. Position the heater directly over the section to be spliced as shown in Positions 1, 4 and 5.

A: Smart Loop belts are supplied with a temporary pin and a permanent pin located in one of the Smart Loops.
- The temporary pin is a 1/8” diameter fiberglass pin for holding the Smart Loop open and preventing damage. (Wider belts may have two pieces instead of one long pin.)
- The permanent pin is a 1/16” diameter Teflon coated piano wire. (It is always one piece.)
It is recommended that two or three people are available for the installation depending on the belt width and general accessibility in the plant environment.
- After the new belt is pulled and in place, remove the temporary splice pin/s. (Fig. 1)
- Overlap the two belt ends. The belt loops must alternate from one end of a belt to the other end of the belt. A small screwdriver or pick may be necessary to stage the splice loops. (Fig. 2 and Fig. 3) Squeeze the splice joint upwards to form an inverted “V”.
- Starting on the side of the belt that the belt tracking sensor is on, begin to reinsert the temporary pin through the loops, pointed side first. (Fig. 4) While one person pushes the pin, another person needs to watch the pin, making sure that the loops are alternating from one side of the belt to the other side of the belt. (Fig. 5)
- Continue this process until the temporary pin is completely installed.
- Next, install the permanent pin from the opposite direction overlapping the temporary pin by approximately 12”. (Fig. 6)
- Carefully pull out the temporary pin from the side it was installed, until an approximate 2” overlay remains with the permanent pin.
- Push the permanent pin in further to again achieve the 12” overlap with the temporary pin. The temporary pin is pulled out to the 2” overlap and this is repeated until the permanent pin if fully inserted.
- After the permanent pin is installed, the overhanging ends (approximately ½” on each end of the belt) of the pin can be bent back in the direction of travel. (Fig. 7).


Let's Get Started on Your New Equipment Project Today.
Let's Get Started
CONNECT WITH OUR EXPERTS
Manufacturing excellence without the one-size-fits-all approach.
We NEVER SETTLE. Neither should you.